What is a high temperature vacuum furnace?
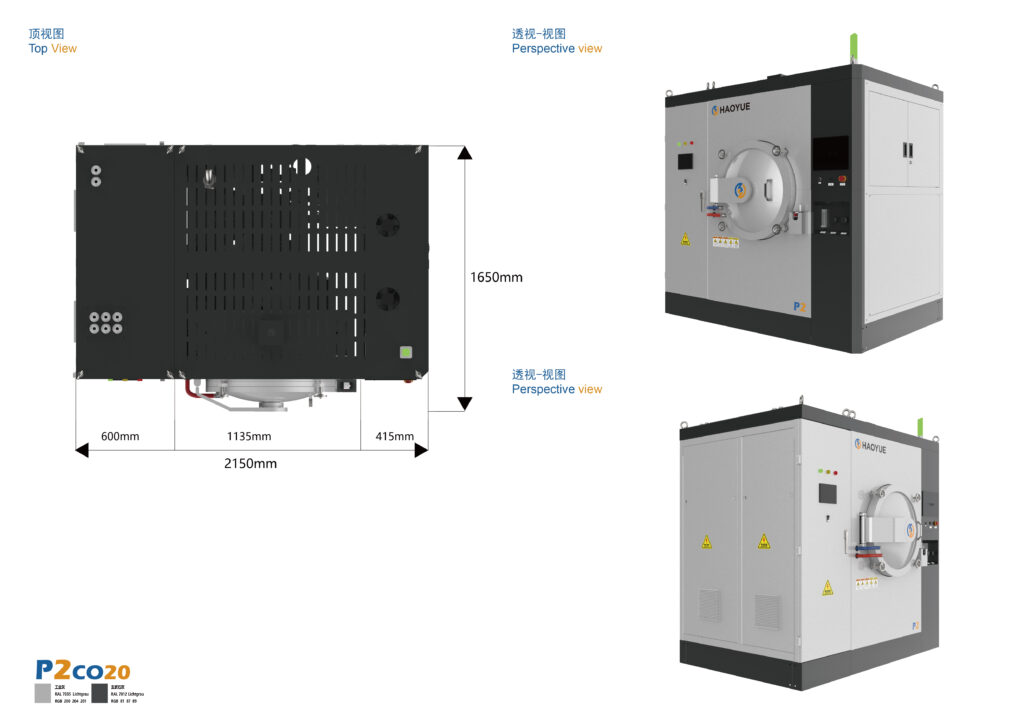
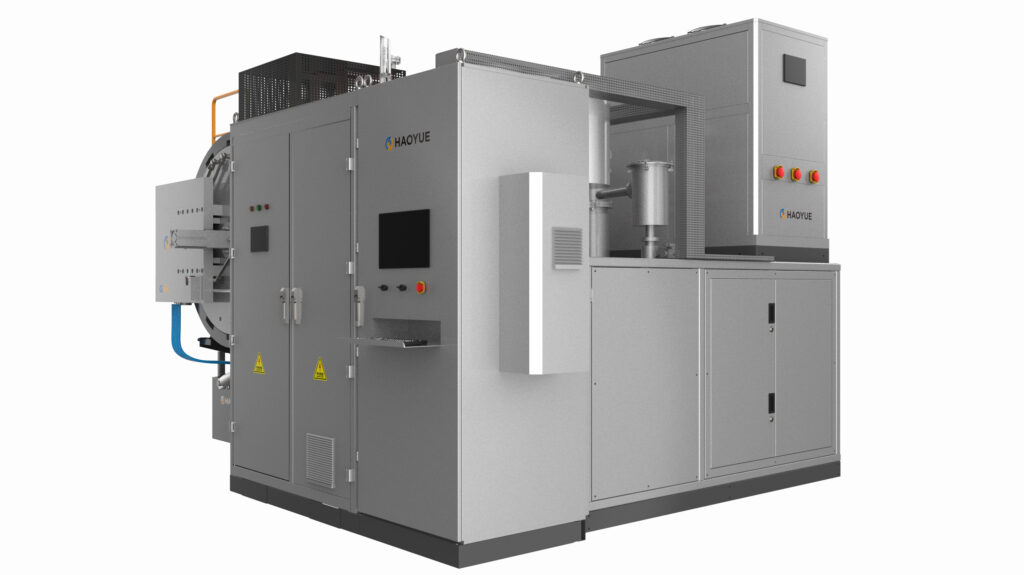
A فرن تفريغ عالي الحرارة is a batch furnace that heats a workload to 1800 °C or above inside a water-cooled chamber held under high vacuum — typically 6.7×10⁻³ Pa when a diffusion or molecular pump is fitted — or under a low partial pressure of inert gas. It exists for one reason: to reach temperatures that oxidise, decarburise or contaminate a material in air, without ever letting oxygen near the part.
The temperature number on a datasheet is the easy part. The engineering question is which منطقة ساخنة — graphite, tungsten or molybdenum — can deliver that number, in your atmosphere, for the number of cycles your production plan actually assumes.
How a high temperature vacuum furnace works
A high temperature vacuum furnace is a system of four sub-systems that must be specified together. Choosing them independently is how projects end up with a furnace that cannot hold its rated temperature.
Stage 1 — Pumping and vacuum level
The chamber is roughed down with a mechanical pump and then brought to high vacuum with a diffusion or molecular pump. In our V-series furnaces the graphite, tungsten and molybdenum hot zones are all rated to 6.7×10⁻³ باسكال in this configuration. Vacuum level is a pump-set decision, not an inherent property of the furnace body: the same chamber ordered with mechanical pumping only reaches the rough-vacuum range (around 1 Pa) and is intended for duties that do not need high vacuum. If your process depends on oxide reduction or on degassing a powder compact, high vacuum is the specification; if it does not, paying for it is optional.
Stage 2 — Heating and the hot zone
Heating elements and insulation define both the ceiling temperature and the atmosphere chemistry the furnace can tolerate. Graphite elements and graphite felt insulation are the workhorse for 2000–2400 °C service in vacuum and inert gas. Tungsten elements suit 1800–2000 °C where carbon contact is unacceptable, and molybdenum covers the 1000–1300 °C band economically.
Stage 3 — Temperature measurement and control
Above roughly 1200 °C a standard thermocouple no longer gives a reliable reading, so high temperature vacuum furnaces switch to optical pyrometry for the upper range and use contact thermocouples only for the lower segment. We build this as a dual-sensor arrangement — a contact sensor for the ramp and a pyrometer for the soak — driven by an industrial computer with PLC and PID control. Temperature uniformity across the useful volume is the metric that matters for part quality: our V-series chambers are mapped at ±5 درجة مئوية using a five-point survey calibrated at 1000 °C.
Stage 4 — Cooling
After the soak the workload has to come down without re-oxidising. An optional 2 bar gas rapid-cooling package circulates inert gas through the hot zone; without it, cooling is by radiation and natural convection only, which can add hours to a cycle.
Key parameters to specify
| المعلمة | لماذا يُعد ذلك مهماً؟ | Typical values in our V-series |
|---|---|---|
| أقصى درجة حرارة | Sets the hot zone material, not just a number | 2000 / 2400 °C (graphite); 1800 / 2000 °C (tungsten); 1000 / 1300 °C (molybdenum) |
| مكنسة كهربائية فائقة الأداء | Governs oxide reduction and degassing | 6.7×10⁻³ Pa (diffusion/molecular pump configuration) |
| Ramp rate | Controls grain growth and thermal shock | 1–15 °C/min below 1600 °C; 1–10 °C/min above 1600 °C |
| تجانس درجة الحرارة | Determines yield across a load | ±5 °C (five-point survey, 1000 °C) |
| Useful chamber size | Sets batch weight and part envelope | 300×300×400 mm up to 800×800×1200 mm |
| تبريد | Cycle time and surface finish | Optional 2 bar gas rapid cooling |
| يتحكم | Reproducibility and traceability | Industrial PC + PLC + PID, multi-zone control |
Two of these deserve emphasis. First, ramp rate is temperature-dependent, not a single figure — a furnace that ramps at 15 °C/min in the lower range will typically be limited to 10 °C/min once above 1600 °C, because radiation losses and element stress both climb. Second, uniformity is a specification you should demand evidence for. A ±5 °C claim is only meaningful next to the survey method and the temperature at which it was taken.
Choosing the hot zone for 1800 °C vs 2300 °C
This is the decision that actually determines whether your furnace works. Graphite, tungsten and molybdenum are not interchangeable options on a price list; each carries an atmosphere limit and a contamination risk.
| منطقة ساخنة | أقصى درجة حرارة | Best fit | Watch out for |
|---|---|---|---|
| الجرافيت (GR) | 2000 / 2400 درجة مئوية | Hardmetals, carbon and graphite products, C/C composites, ceramics that tolerate carbon | Carbon pick-up on carbon-sensitive alloys; not for oxidising atmospheres |
| Tungsten (W) | 1800 / 2000 درجة مئوية | Refractory metals, transparent and technical ceramics, carbon-free sintering | Higher cost; avoid oxidising and moisture-rich atmospheres |
| Molybdenum (MO) | 1000 / 1300 درجة مئوية | Non-ferrous metals, stainless and titanium alloys, high-speed steel, hydrogen-sensitive work | Lower ceiling; not the choice when 1800 °C+ is the target |
| Induction graphite (CO) | 2000 / 2400 درجة مئوية | Large-section graphite and carbon parts needing fast cycles | 5 Pa vacuum configuration; induction field considerations |
| Continuous graphite (CGR) | 2000 °C | Volume production of uniform parts | 10 Pa vacuum configuration; suited to line production, not one-off runs |
The practical rule: if you need 2300 °C, you need a graphite hot zone. If you need 1800 °C and the material cannot touch carbon, you need tungsten. Molybdenum is the economical answer only when the process ceiling sits at or below 1300 °C.
Available high temperature vacuum furnace models
Our V-series covers the 1800–2400 °C band with matched chamber sizes, so the hot zone and the useful volume can be selected independently.
| نموذج | منطقة ساخنة | حجم الحجرة (مم) | مكنسة كهربائية فائقة الأداء | أقصى درجة حرارة |
|---|---|---|---|---|
| V3GR24 | الجرافيت (GR) | 300×300×400 | 6.7×10⁻³ باسكال | 2000 / 2400 درجة مئوية |
| V4GR24 | الجرافيت (GR) | 400×400×600 | 6.7×10⁻³ باسكال | 2000 / 2400 درجة مئوية |
| V6GR24 | الجرافيت (GR) | 600×600×900 | 6.7×10⁻³ باسكال | 2000 / 2400 درجة مئوية |
| V7GR24 | الجرافيت (GR) | 700×700×1000 | 6.7×10⁻³ باسكال | 2000 / 2400 درجة مئوية |
| V8GR24 | الجرافيت (GR) | 800×800×1200 | 6.7×10⁻³ باسكال | 2000 / 2400 درجة مئوية |
| V3W20 | Tungsten (W) | 300×300×400 | 6.7×10⁻³ باسكال | 1800 / 2000 درجة مئوية |
| V4W20 | Tungsten (W) | 400×400×600 | 6.7×10⁻³ باسكال | 1800 / 2000 درجة مئوية |
| V5W20 | Tungsten (W) | 500×500×700 | 6.7×10⁻³ باسكال | 1800 / 2000 درجة مئوية |
| V6W20 | Tungsten (W) | 600×600×900 | 6.7×10⁻³ باسكال | 1800 / 2000 درجة مئوية |
| V4M013 | Molybdenum (MO) | 400×400×600 | 6.7×10⁻³ باسكال | 1000 / 1300 درجة مئوية |
| V8M013 | Molybdenum (MO) | 800×800×1200 | 6.7×10⁻³ باسكال | 1000 / 1300 درجة مئوية |
| V6CO24 | Induction graphite | 600×600×900 | 5 باسكال | 2000 / 2400 درجة مئوية |
| V6CGR20 | Continuous graphite | 600×600×900 | 10 باسكال | 2000 °C |
All V-series furnaces share the same control platform, five-point ±5 °C uniformity mapping, multi-zone temperature control and the optional 2 bar rapid-cooling package. See the full vacuum sintering furnace range for chamber details and loading configurations.
High temperature vacuum furnace vs alternative processes
Temperature alone rarely decides the process. Pressure, atmosphere and cycle shape usually matter just as much.
| عملية | Temperature capability | Pressure / atmosphere | اختره عندما |
|---|---|---|---|
| High temperature vacuum furnace | 1800–2400 °C | Vacuum (6.7×10⁻³ Pa) or partial pressure | You need the highest temperature with no carbon or oxygen contamination |
| الضغط الساخن بالتفريغ | 2200 درجة مئوية | Uniaxial pressure, 100–1200 t | You need densification, not just heating — pressure closes porosity |
| Spark plasma sintering (SPS) | 2200 درجة مئوية | Uniaxial, very fast ramps (up to 300 °C/min) | You need to suppress grain growth in a laboratory or pilot scale |
| Gas pressure sintering (GPS) | 1600 / 2000 درجة مئوية | 6 / 10 MPa inert gas | You need isostatic-like densification of ceramics without a pressure head |
| Diffusion bonding furnace | 1400 °C | Vacuum, mechanical pressure | You are joining parts and 1400 °C is sufficient |
| فرن هيدروجين فراغي | 1000 / 1300 درجة مئوية | Vacuum + hydrogen | You need oxide reduction in a reducing atmosphere |
For densification with pressure at ultra-high temperature, our P-series graphite vacuum hot pressing furnace reaches 2200 °C with 100–1200 t of uniaxial force. For volume production of small, uniform parts, a continuous multi-station platform may beat a batch furnace on cost per part.
التطبيقات
- Hardmetals and cemented carbide — sintering and post-sintering heat treatment on graphite hot zones.
- Transparent and technical ceramics — Al₂O₃, ZrO₂, Si₃N₄, SiC where a carbon-free tungsten hot zone protects optical and electrical properties.
- Refractory metals — tungsten, molybdenum and their alloys, sintered or annealed in the hot zone that can hold the temperature.
- Carbon and graphite products — electrodes, C/C brake discs and plates, graphite felt, thermally conductive film.
- Powder metallurgy and MIM — debinding plus vacuum sintering with optional hydrogen pre-treatment.
- مواد الفضاء الجوي وأشباه الموصلات — high-melting-point and high-purity work that tolerates neither oxygen nor carbon.
Limitations — when not to choose a high temperature vacuum furnace
A 2400 °C furnace is the wrong purchase more often than buyers expect. Be honest about these cases:
- You do not actually need 1800 °C. If the process tops out at 1300 °C, a molybdenum hot zone or a dedicated vacuum hydrogen furnace costs less to buy and less to run.
- You need pressure, not just temperature. Vacuum alone cannot close residual porosity in many ceramics; that is a hot pressing or GPS job.
- Your material cannot see carbon. Above 1800 °C the practical hot zone is graphite unless you move to tungsten, and tungsten raises the cost of both the furnace and the elements.
- You need fast cycle times on small parts. Batch vacuum cycles include pump-down and controlled cooling; a continuous platform will generally win on throughput.
- Your atmosphere must be reducing, not vacuum. Hydrogen-related reduction and brazing belong in a hydrogen furnace, not a high vacuum chamber.
- You cannot support the utilities. High vacuum needs diffusion or molecular pumping, and 2400 °C imposes real power and water-cooling loads on the building.
التعليمات
What is the difference between 1800 °C and 2300 °C in practice?
It is a hot zone material decision, not a set-point. Above 2000 °C the graphite hot zone is the standard route; 1800 °C can also be reached with a tungsten hot zone, which avoids carbon contact but costs more.
What vacuum level does a high temperature vacuum furnace need?
High vacuum — 6.7×10⁻³ Pa with a diffusion or molecular pump — is the configuration we supply for V-series furnaces. Lower-cost mechanical pumping only reaches the rough-vacuum range and is intended for duties that do not require high vacuum.
How fast can a high temperature vacuum furnace heat up?
Typically 1–15 °C/min below 1600 °C and 1–10 °C/min above 1600 °C. Induction-heated graphite furnaces in the same series allow faster ramps, up to 60 °C/min in the lower range.
What temperature uniformity should I expect?
We map ±5 °C across the useful volume using a five-point survey calibrated at 1000 °C. Ask any supplier for the survey method and the reference temperature behind their uniformity claim.
Can a high temperature vacuum furnace run with a partial pressure of inert gas?
Yes. Partial-pressure operation is common when a fully evacuated chamber would volatilise an element of the charge; it is a standard control option rather than a separate furnace design.
When should I choose hot pressing or gas pressure sintering instead?
When the goal is densification rather than heat treatment. Uniaxial hot pressing reaches 2200 °C with 100–1200 t of force, and gas pressure sintering applies 6/10 MPa of inert gas for near-isostatic densification of ceramics.